- توربو
- مدونة
ESD glove lot traceability connects the gloves used at a workstation to the approved product, incoming shipment and release decision. Keep the supplier lot identity through receiving, storage, repacking and issue, then record enough information to locate affected stock if a concern emerges. A carton number alone is insufficient when cartons are split without a corresponding record. Traceability also does not prove electrical performance: it tells you which evidence and which material belong together. For electronics manufacturers, the practical goal is a usable chain of identity that supports controlled purchasing and a focused investigation without forcing operators to complete unnecessary paperwork.
Define the identity chain before ordering
Start with the supplier product designation and your internal approved item number. Record the glove construction, ordered size and relevant drawing or specification revision. A supplier batch may cover several cartons, while a shipment may contain several batches. Ask the supplier how these relationships are represented rather than assuming that the purchase order, delivery date and manufacturing lot mean the same thing. If different sizes have separate identities, retain those differences when the stock is issued.
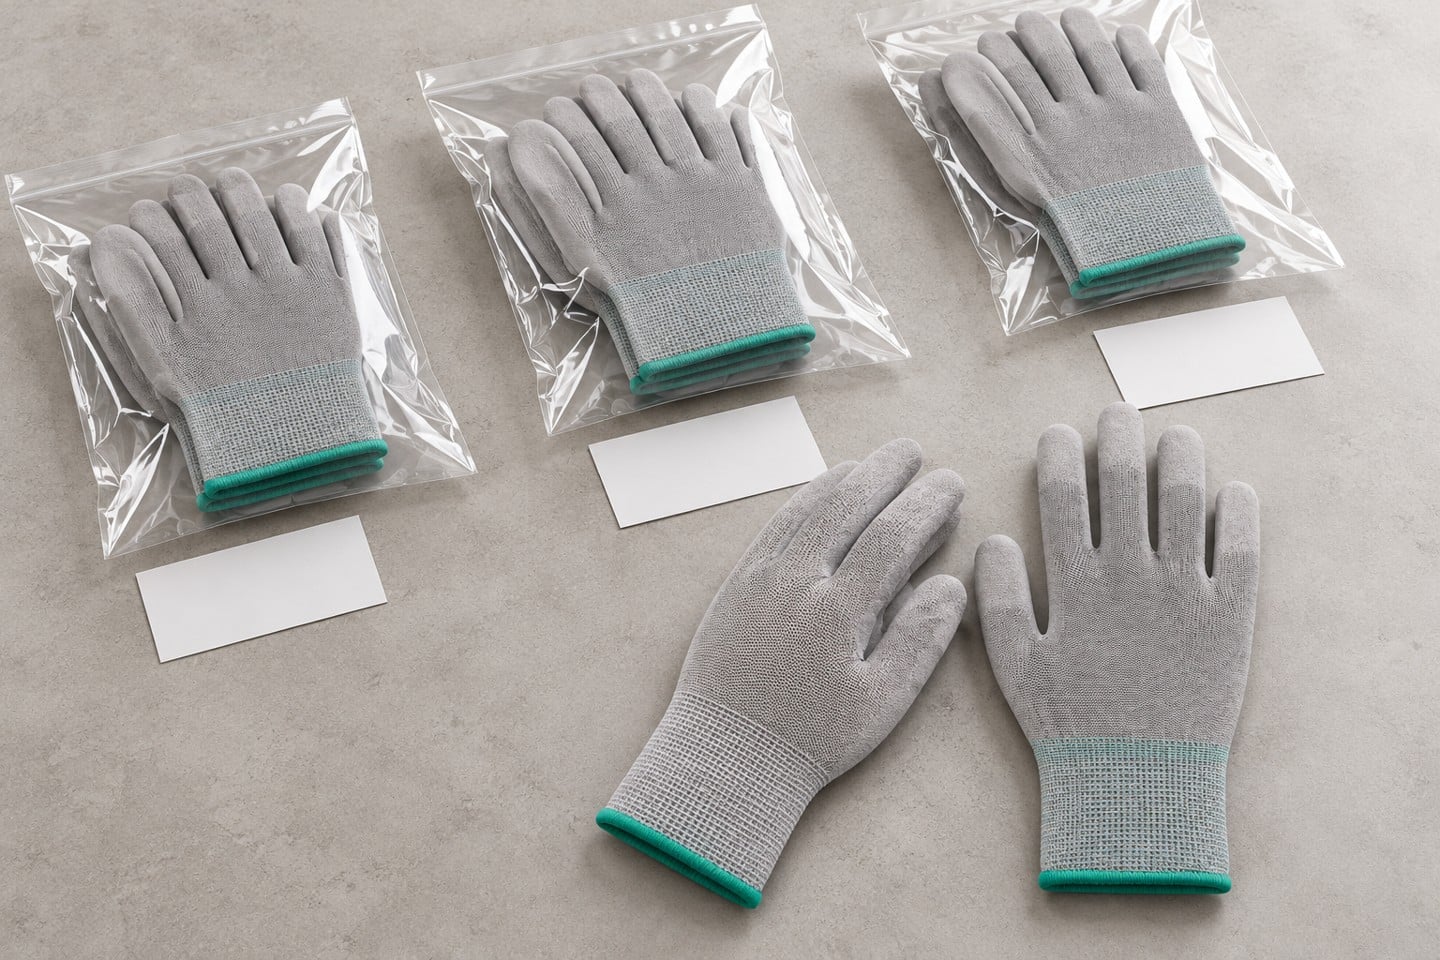
For example, the SWESD carbon-fiber PU palm-coated glove gives purchasing a specific product reference to discuss. Its product photograph identifies the visible construction; it does not establish your required test outcome, packaging quantity or supplier traceability system. Put those requirements into the quotation and approval exchange. Obtain a sample label or document layout before committing to a record structure that the supplier cannot support.
Separate identification from qualification
An approved sample establishes a reference only within the evaluation that was actually performed. A later delivery bearing the same trade name may still require checks against the purchasing specification. Link the sample approval, relevant test documentation, supplier designation and lot information through controlled records. Follow the ESD test report review guide when deciding whether evidence describes the actual submitted product and applicable conditions.
ال EOS/ESD Association overview of control procedures and materials explains the broader control-program context. Lot records support that program but cannot replace its technical requirements. Do not describe a batch as electrically acceptable merely because its code matches an invoice. Define who reviews performance evidence and who releases incoming stock, especially when those responsibilities sit in different departments.
Check incoming cartons before splitting them
At receiving, compare the physical product and supplier labels with the purchase documents. Record the supplier lot exactly, including prefixes, separators and leading zeroes. If the label is unclear, preserve a photograph within the controlled record and request clarification. Do not create an apparently precise lot by combining unrelated delivery information. Your internal receiving identifier can be added alongside the original identity, provided the relationship is explicit and retrievable.
Inspect all represented sizes and lots according to the approved receiving plan. One photographed carton does not establish the identity of every carton in a mixed shipment. Where supplier labels exist only on the outer package, decide how identity will survive opening before moving material into smaller bins. Hold material with conflicting or absent identification for an authorized decision. Urgent production demand is a reason to escalate the decision promptly, not to erase the uncertainty.
Use a short record that follows real movements
| Stage | Keep connected | Decision supported |
|---|---|---|
| موافقة | Item designation, specification and reviewed evidence | Which construction was accepted? |
| Receiving | Supplier lot, size, shipment and receiving identity | What material arrived? |
| Repacking | Source lot and new container identity | Can a split carton still be traced? |
| Issue | Lot, station or approved production reference | Where could material have been used? |
| Investigation | Observed condition and affected identities | What stock and records need review? |
These are record-design choices, not universal mandatory fields or acceptance limits. Select the smallest set that allows your team to answer which approved material was received, where it went and what should be checked if a concern arises. A simple controlled register can be more reliable than a complicated system with fields that people routinely guess. Test the register using a real split-carton example before rolling it out to all lines.
Keep revision control separate from the lot field. A change in the approved glove specification should remain visible even if the supplier happens to retain a familiar product name. Similarly, a partial return needs its original identity and a clear condition status. A return transaction should never silently convert used, uncertain or uninspected gloves into new approved stock.
Preserve identity when repacking and issuing
When transferring gloves into a smaller package, use a durable internal label that points back to the source lot and receiving record. Keep different lots separate unless the approved system can identify every constituent lot and support a sensible response later. Avoid topping up a bin indefinitely: that practice makes the bin label increasingly detached from the contents. Empty, inspect and relabel the bin under a defined process before introducing a replacement lot.
At line issue, choose a record granularity proportional to the consequence of losing identity. Some operations can trace by issue period and workstation; others need a connection to a production order or controlled assembly batch. This is a process decision, not a promise that individual gloves carry unique identities. Record the actual level supported by your workflow. When operators move between stations, verify that the chosen method still reflects where material was used.
Keep size and operator suitability visible
A correct lot does not make an unsuitable glove size acceptable. Keep size information with the issue identity and prevent substitutions based only on what is available in the cabinet. The glove sizing and dexterity guide addresses fit and handling, which remain separate decisions. If an operator changes size or construction, record the issue correctly and use the established approval route for any change that affects the qualified task.
Similarly, palm-coated and fingertip-coated versions should not be treated as interchangeable stock merely because they appear in the same product family. The palm versus fingertip coating comparison explains the handling boundary. Preserve the exact approved designation in stock records so that a database shortcut does not conceal a construction change. Treat relabelled substitutions as changes requiring review rather than as clerical corrections.
Run a retrieval drill before a real incident
Select an issued lot and ask a colleague to find its incoming record, release evidence and remaining stock locations. Then reverse the exercise: start with a supplier lot and determine which issue records could be affected. Record what could actually be retrieved and what remained uncertain. Do not mark the drill successful just because somebody remembers where the carton was stored. The method must work when the usual storekeeper is absent.
ال EOS/ESD Association discussion of training and auditing provides useful background for checking whether documented controls are implemented. Train staff using the actual labels, bins and exception routes they encounter. A record check should look for consistent execution and meaningful gaps, not just completed boxes. Repeat the exercise after significant changes to labels, suppliers, storage systems or issue practices.
Respond to a suspected lot concern
When a defect or performance question is raised, preserve the observed condition and identity first. Record the workstation, issue period, task and available supporting evidence. Segregate implicated remaining material according to your process and involve the authorized quality and ESD personnel. The traceability chain narrows the investigation; it does not establish that the glove caused the event or that every item in a batch has the same condition.
If records cannot distinguish between two lots, make that uncertainty visible in the investigation scope. Avoid narrowing the affected population using assumptions about normal stock rotation. Ask the supplier for clarification with the original labels and purchasing references attached through your controlled communication process. Document the final disposition and any corrective change to receiving or issue controls, so the same identity gap does not recur on the next delivery.
Put practical requirements into the RFQ
Ask how manufacturing lots, size variants, cartons and individual packs are identified. Request a representative label, an explanation of mixed shipments and the available connection between supplied material and supporting documentation. Define whether advance notice is needed for changes to construction, labelling or manufacturing source. Do not request an unsupported blanket guarantee that the supplier cannot substantiate. A clear evidence request makes quotations easier to compare and incoming decisions easier to execute.
Agree the response needed when labels are damaged or information conflicts. Include your preferred contact path, document references and the person authorized to release held material. Trial the arrangement on the first delivery and improve fields that create confusion. The useful outcome is a repeatable identity chain from approval to line issue, supported by technical checks appropriate to the application, rather than a large archive of disconnected invoices and sample reports.
Electrical-control background
The following EOS/ESD Association educational video supplies background on ESD control. It is not a tutorial on supplier lot numbering and does not certify the illustrated gloves. Use it alongside your approved control plan to explain why identity and technical acceptance must remain connected while being assessed separately.
الأسئلة الشائعة
Does a supplier lot number prove ESD performance?
No. Identity connects material to evidence; electrical acceptance needs the applicable qualification and verification.
Is the purchase order number a manufacturing lot?
Not necessarily. Ask the supplier how purchase orders, shipments, cartons and manufacturing lots are related.
Can different lots share one issue bin?
Keep them separate unless the approved record system identifies every constituent lot and supports an effective investigation.
Must every glove have a unique serial number?
No. Choose an achievable traceability level appropriate to the process and record its actual limits.
What should happen when a lot label is unreadable?
Hold the affected material for an authorized clarification while preserving the original label and shipment information.
أحدث مشاركة
-
 ESD Glove Lot Traceability from Approval to Line Issue28 أكتوبر,2026
-
 Protecting SMT Reel Leader Tape During Tray Transport27 أكتوبر,2026
-
اترك ردًا