- Turbo
- Blog
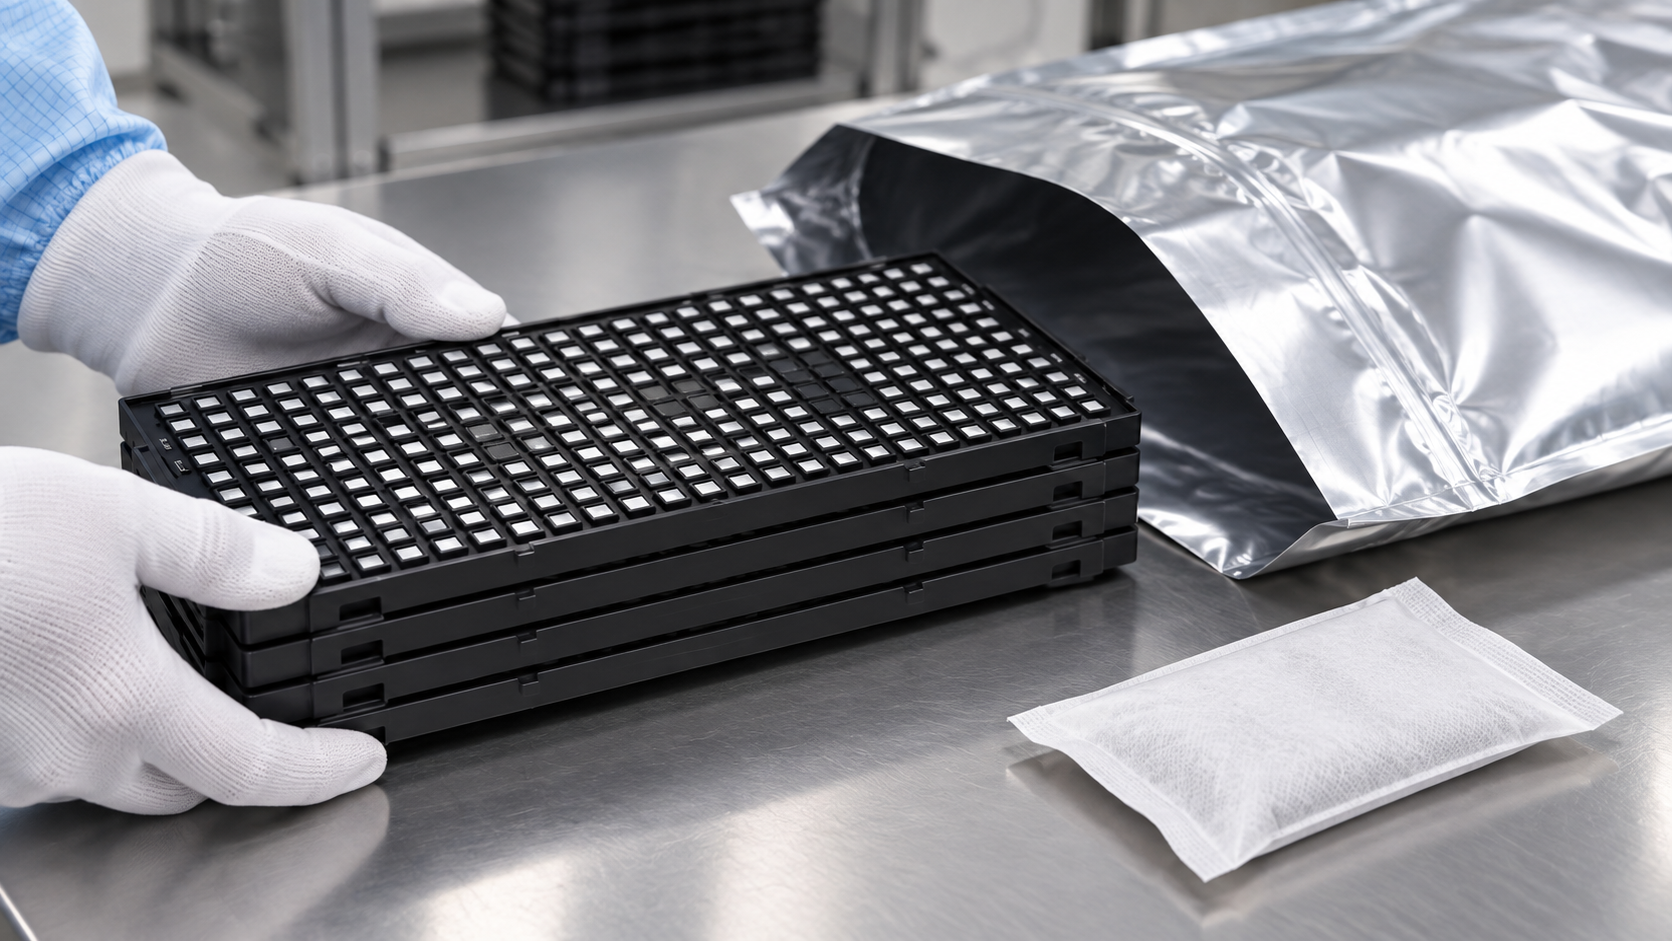
IC Tray Packaging for Moisture-Sensitive Devices is a purchasing and validation problem: the aim is to integrate tray stacks into a moisture-control pack without assuming the tray alone protects moisture-sensitive devices. A reliable decision starts with the protected device and its complete route, then converts the search term into measurable drawing, sample and receiving requirements. There is no universal material, tolerance, reuse count or test value that safely fits every program.
Decision Summary for ic tray packaging
| Decision area | Define before quotation | Evidence to request |
|---|---|---|
| Device status | MSL, exposure history and allowed floor life | Follow the component and process control documents |
| Barrier system | Moisture-barrier bag, desiccant and indicator | Use qualified materials and sealing process |
| Tray heat exposure | Any bake condition before packing | Verify the exact tray material and stack |
| Labeling | Moisture status, lot and opening instructions | Keep records aligned with the sealed pack |
Use the table as an RFQ discussion guide, not as a substitute for controlled values. Final limits should come from current device drawings, equipment interfaces, the facility ESD program, supplier documentation and qualified trials. When a number is not yet known, state the functional risk and agree a prototype test instead of copying a limit from an unrelated tray.
1. Device status: Turn the Requirement into Evidence
For ic tray packaging, the buyer must define msl, exposure history and allowed floor life. This point controls whether the tray can integrate tray stacks into a moisture-control pack without assuming the tray alone protects moisture-sensitive devices. Write the requirement against the actual device, route and equipment rather than a generic tray description. Name the responsible drawing or work instruction, the condition in which the characteristic applies, and who approves an exception.
The practical verification is to follow the component and process control documents. Begin with identified samples from the proposed production material and tooling. Record sample quantity, lot or cavity, conditioning, equipment, method and result. Include both normal and credible worst-case conditions. A pass on one convenient sample is useful for development, but it is not evidence that production variation is controlled.
Ask the supplier to explain which input variables can change this result. Depending on the characteristic, these may include resin or sheet lot, additive level, molding or forming settings, cooling, trimming, storage, cleaning and previous use. Convert important variables into incoming evidence, periodic checks or formal change notification. This makes the requirement auditable and prevents a catalog promise from becoming the only acceptance basis.
2. Barrier system: Turn the Requirement into Evidence
For ic tray packaging, the buyer must define moisture-barrier bag, desiccant and indicator. This point controls whether the tray can integrate tray stacks into a moisture-control pack without assuming the tray alone protects moisture-sensitive devices. Write the requirement against the actual device, route and equipment rather than a generic tray description. Name the responsible drawing or work instruction, the condition in which the characteristic applies, and who approves an exception.
The practical verification is to use qualified materials and sealing process. Begin with identified samples from the proposed production material and tooling. Record sample quantity, lot or cavity, conditioning, equipment, method and result. Include both normal and credible worst-case conditions. A pass on one convenient sample is useful for development, but it is not evidence that production variation is controlled.
Ask the supplier to explain which input variables can change this result. Depending on the characteristic, these may include resin or sheet lot, additive level, molding or forming settings, cooling, trimming, storage, cleaning and previous use. Convert important variables into incoming evidence, periodic checks or formal change notification. This makes the requirement auditable and prevents a catalog promise from becoming the only acceptance basis.
3. Tray heat exposure: Turn the Requirement into Evidence
For ic tray packaging, the buyer must define any bake condition before packing. This point controls whether the tray can integrate tray stacks into a moisture-control pack without assuming the tray alone protects moisture-sensitive devices. Write the requirement against the actual device, route and equipment rather than a generic tray description. Name the responsible drawing or work instruction, the condition in which the characteristic applies, and who approves an exception.
The practical verification is to verify the exact tray material and stack. Begin with identified samples from the proposed production material and tooling. Record sample quantity, lot or cavity, conditioning, equipment, method and result. Include both normal and credible worst-case conditions. A pass on one convenient sample is useful for development, but it is not evidence that production variation is controlled.
Ask the supplier to explain which input variables can change this result. Depending on the characteristic, these may include resin or sheet lot, additive level, molding or forming settings, cooling, trimming, storage, cleaning and previous use. Convert important variables into incoming evidence, periodic checks or formal change notification. This makes the requirement auditable and prevents a catalog promise from becoming the only acceptance basis.
4. Labeling: Turn the Requirement into Evidence
For ic tray packaging, the buyer must define moisture status, lot and opening instructions. This point controls whether the tray can integrate tray stacks into a moisture-control pack without assuming the tray alone protects moisture-sensitive devices. Write the requirement against the actual device, route and equipment rather than a generic tray description. Name the responsible drawing or work instruction, the condition in which the characteristic applies, and who approves an exception.
The practical verification is to keep records aligned with the sealed pack. Begin with identified samples from the proposed production material and tooling. Record sample quantity, lot or cavity, conditioning, equipment, method and result. Include both normal and credible worst-case conditions. A pass on one convenient sample is useful for development, but it is not evidence that production variation is controlled.
Ask the supplier to explain which input variables can change this result. Depending on the characteristic, these may include resin or sheet lot, additive level, molding or forming settings, cooling, trimming, storage, cleaning and previous use. Convert important variables into incoming evidence, periodic checks or formal change notification. This makes the requirement auditable and prevents a catalog promise from becoming the only acceptance basis.
Prototype and Production Approval
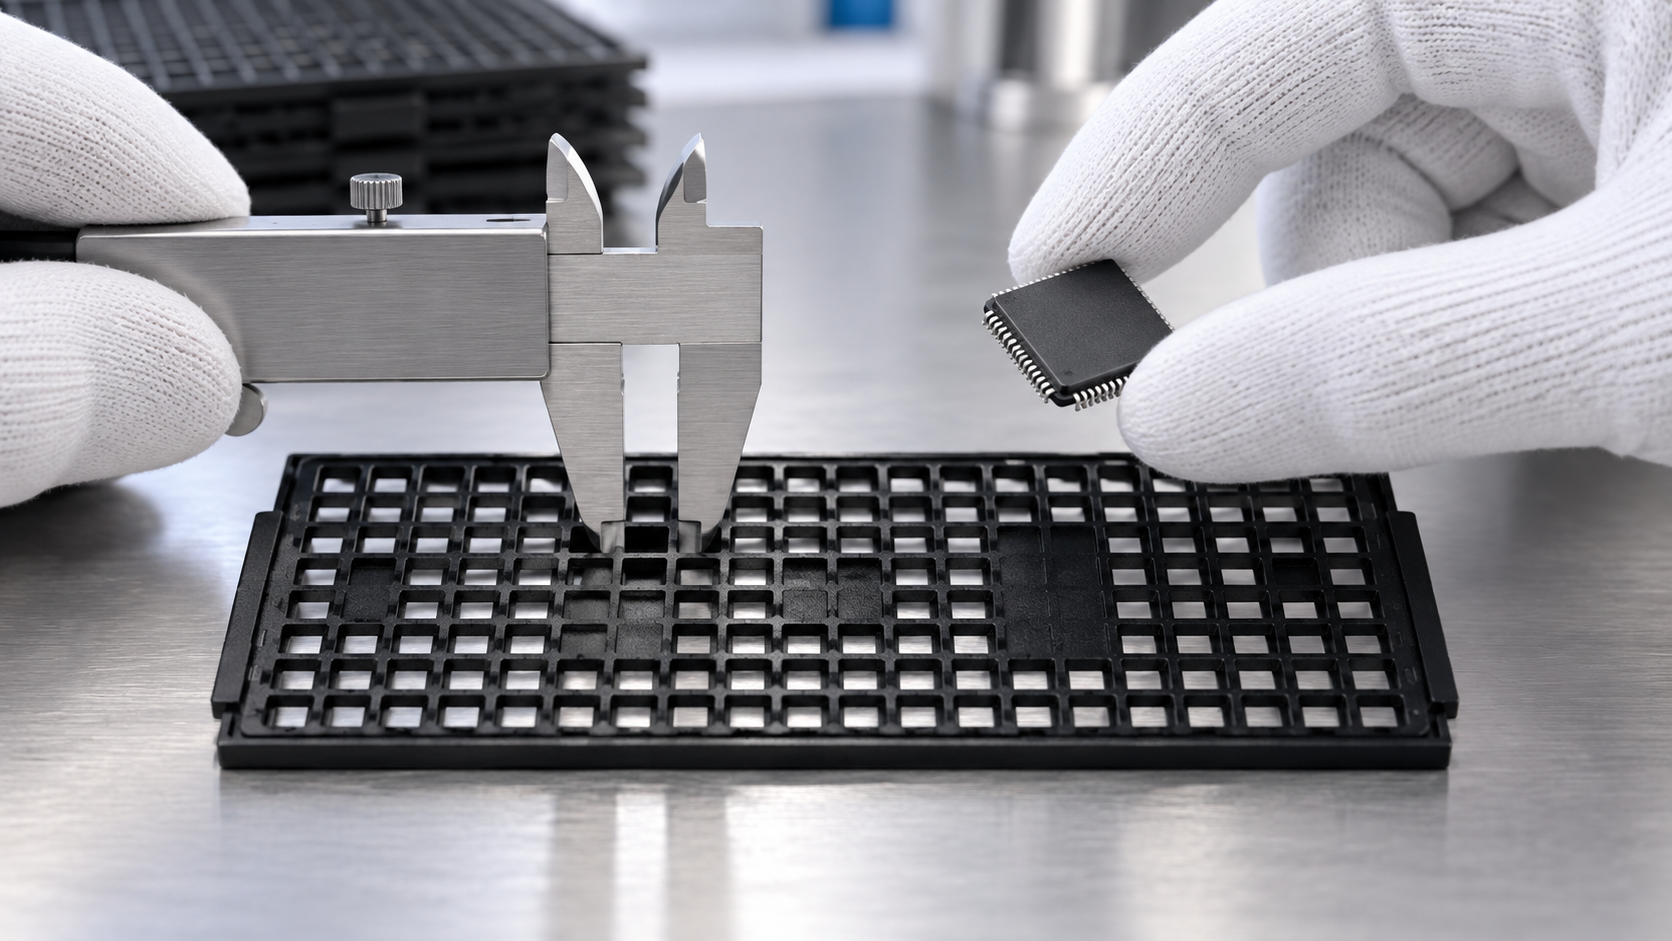
Approve the proposal in gates. First review the device revision, orientation, allowed contact, route, equipment and packaging stack. Next inspect identified first articles and verify the four decision areas above. Then load representative minimum and maximum devices, build the real stack, apply covers or restraints, and run the normal handling sequence. Include cleaning, heat, labels, storage and shipment only where they belong to the actual route.
Keep the approved drawing, material or construction identity, sample lot, photographs, raw results, deviations and sign-off together. Receiving inspection should check identity before sampling, separate lots, inspect critical features with the approved datum and method, and quarantine failures before they mix with accepted inventory. Sampling depth follows risk and supplier history; it should not be invented in a blog or purchase note.
Failures That the Control Plan Must Prevent
Failure 1: Treating a black tray as a moisture barrier
This shortcut can release trays that look acceptable but fail during handling. Contain the affected lot, identify where the assumption entered the specification, and compare the tray with the controlled device and process requirements. Repeat the relevant dimensional, functional or electrical check under documented conditions. Record the disposition so the same issue can be recognized at receiving and during reuse.
Failure 2: Baking trays at a device profile without tray approval
This shortcut can release trays that look acceptable but fail during handling. Contain the affected lot, identify where the assumption entered the specification, and compare the tray with the controlled device and process requirements. Repeat the relevant dimensional, functional or electrical check under documented conditions. Record the disposition so the same issue can be recognized at receiving and during reuse.
Failure 3: Sealing warm or wet materials into the bag
This shortcut can release trays that look acceptable but fail during handling. Contain the affected lot, identify where the assumption entered the specification, and compare the tray with the controlled device and process requirements. Repeat the relevant dimensional, functional or electrical check under documented conditions. Record the disposition so the same issue can be recognized at receiving and during reuse.
RFQ and Supplier Checklist
- Controlled device drawing, samples, orientation and surfaces that may contact the pocket.
- Tray quantity, stack quantity, cover, restraint, outer packaging and equipment interfaces.
- The four topic-specific decision areas and the exact evidence expected for each.
- Material or construction identity, restricted substances, cleaning and environmental exposure.
- First-article quantity, production-lot traceability, inspection method and retention records.
- Change notification for material, additive, coating, tool, cavity, site, process or subcontractor.
- Reuse inspection, obsolete-label control, cleaning instructions and retirement criteria where applicable.
Start the commercial discussion from SWESD’s IC tray product page. For adjacent decisions, consult the JEDEC tray dimensions guide, custom IC tray RFQ guide and semiconductor shipping tray guide. These pages support planning; the controlled project documents remain decisive.
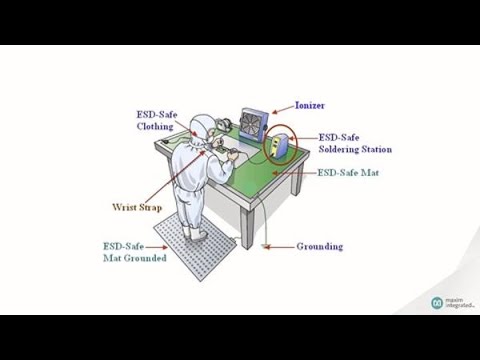
Educational Video: ESD Context
This neutral manufacturer video explains electrostatic-discharge fundamentals. It is supplementary and does not set project-specific tray limits.
Frequently Asked Questions
Does a JEDEC tray stop moisture?
No. Moisture protection normally depends on the qualified barrier package and process. The approved answer should identify the applicable device, tray revision, route and evidence so that purchasing and production use the same rule.
Can devices be baked in any tray?
No. Verify the exact tray material, temperature, duration, load and stack condition. The approved answer should identify the applicable device, tray revision, route and evidence so that purchasing and production use the same rule.
What belongs inside the barrier bag?
Only components and qualified packing materials defined by the process. The approved answer should identify the applicable device, tray revision, route and evidence so that purchasing and production use the same rule.
When should the bag be sealed?
After the approved preparation and within the controlled exposure window. The approved answer should identify the applicable device, tray revision, route and evidence so that purchasing and production use the same rule.
How should receiving handle a damaged bag?
Quarantine and evaluate moisture history under the approved material-control process. The approved answer should identify the applicable device, tray revision, route and evidence so that purchasing and production use the same rule.
Authoritative References
- EOS/ESD Association: packaging and material-handling fundamentals
- NASA-STD-8739.6B: Electrostatic Discharge Control
- JEDEC JEP95: registered and standard mechanical outlines
Application boundary: Final dimensions, electrical limits, temperature exposure, inspection frequency and disposition rules must follow current controlled drawings, standards, manufacturer information and the facility quality and ESD systems.
Leave a Reply